Low pressure die casting is a metal forming process in which molten metal is pumped into a die cavity from a sealed holding furnace by means of a regulated pressure of gas. This method controls the metal supply, during the filling and solidification process. Gravity casting depends primarily on gravity to fill the mold. Flow control may improve casting uniformity, and careful management of equipment and process parameters may reduce turbulence and restrict the entrainment of oxide layer. Low pressure die casting offers an attractive tradeoff in dimensional control, material efficiency and production repeatability for manufacturers of aluminum housings, automobile structural components, motor parts and other precision metal goods. But the final product depends on a lot more than the casting equipment. The quality of the component is affected by the selection of alloy, the design of the die and control of die temperature, the feeding conditions, the cooling rates and the treatments after casting. This knowledge allows the engineer to judge the feasibility of the process for a given product and to establish realistic manufacturing requirements.
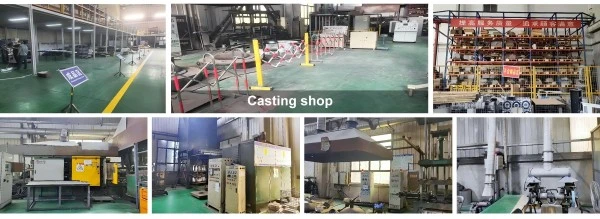
Understanding How Low Pressure Die Casting Works
The Principle Behind Controlled Metal Filling
In the standard low-pressure die-casting method, the molten metal is stored in a sealed furnace in or near the die assembly. The die is attached to the furnace by a riser tube. A regulated gas pressure is applied to the surface of the molten metal. This pressure forces the liquid metal up the tube and into the mold chamber.
The pressure is changed slowly to manage the filling rate. The mechanism maintains appropriate pressure throughout the solidification of the metal when the cavity is filled up. This feeding action can compensate for solidification shrinkage as long as the feeding channel is functional and the process is adequately organized.
When enough solidification has occurred, the pressure is released and the casting removed from the die. Depending on the application of the component, it could be subjected to trimming, machining, heat treatment, surface finishing, inspection, etc.
The main advantage of this set-up is the possibility to control the molten metal distribution into the cavity. A stable filling pattern reduces some flow-related defects and promotes uniform manufacturing. But that doesn't necessarily mean no porosity, no inclusions, and no dimension fluctuation. These difficulties still need good process design and quality control to solve.
How It Differs From Other Casting Methods?
There is high-pressure die casting and gravity die casting but also low-pressure die casting. Gravity die casting largely relies on the weight of the metal to fill the mold and so is suitable for a broad variety of very simple or rather complex parts. Low-pressure die casting is filling and feeding with controlled pressure. This can result in an enhanced process stability for the adequate geometries.
In high-pressure die casting, the molten metal is forced into the die by a piston at pressures significantly higher than in low-pressure die casting and usually at high filling rates. It is ideally suited for short production runs and complex thin-wall parts, but the quick-filling conditions necessitate careful management of gas entrapment and other process difficulties.
Low-pressure die casting is frequently used for the production of components needing a good internal structure, uniform wall thickness, and adequate mechanical properties. The best technique is still dependent on the volume of production, geometries, needs of the alloy, tooling investment, dimensional tolerances, and acceptance criteria of the customer.
Equipment and Process Control
The Main Components of a Casting System
The basic low pressure die casting machine consists of a holding furnace, riser tube, pressure regulation system, die assembly, cooling circuits, and methods of opening the die and retrieving the final casting. Automated controls and robotic handling equipment may also be included, depending on the production line.
The holding furnace shall maintain the alloy in the proper temperature range and shall prevent oxidation and contamination. Design and operation parameters will determine the melt stability, cleanliness of the metal, and homogeneity of the material fed to the die.
The connection from the furnace to the mold is called the riser tube. The transmission of metal is influenced by metal composition, size, sealing arrangement, and maintenance condition. The pressure control device controls the gas pressure profile during filling, holding, and pressure release.
The die controls the geometry of the part but also affects the flow and solidification of the metal. The shape and functional requirements of the casting affect the design of the venting, cooling, parting line, and ejector features. Even if the equipment is operating within rated limitations, problems can arise if the cooling channels are improperly located or if there is insufficient venting.
Managing Temperature, Pressure, and Filling Time
We define the desired conditions for the selected alloy and part to begin the process control. The temperature of the metal should be sufficiently high to keep the metal fluid during filling. If the temperature is too high or the hold times are longer than necessary, quality problems like oxidation and gas absorption can arise.
Another critical variable is pressure. The pressure profile should be strong enough to fill the cavity but not so powerful that the flow pattern becomes unstable. The pressure and time of holding must be sufficient to support the feed as the metal cools and solidifies after filling. Premature pressure release may cause the feeding to stop, and wrong pressure settings may cause the process instability.
The time of filling is determined by the capacity of the cavity, the wall thickness, the flow resistance, and the gating system parameters. The thin parts may be troublesome, as they may set before the depression is entirely filled. However, fast filling may increase the turbulence and the tendency to entrap the oxide layer.
Instead of one set of parameters for all components, producers need to build a process window through engineering study, trial castings, and production validation. As evidence for the determination of the process stability throughout multiple production runs, temperature records, pressure curves, cycle data, and inspection findings are employed.
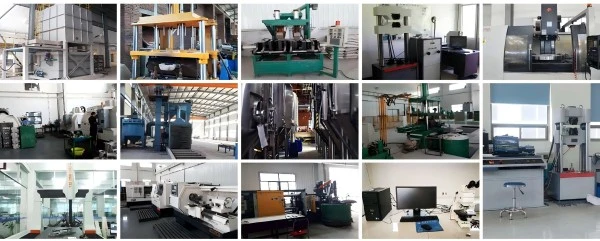
Choosing Materials and Designing the Casting
Aluminum Alloys and Other Suitable Metals
Aluminum alloys are exploited in low pressure die casting owing to their low density, excellent mechanical properties, and range of component geometries. Typical cast alloys are A356 and A357; however, the right grade is chosen based on the needed strength, ductility, corrosion resistance, heat treatment reaction, and applicable standards.
A356 is a common alloy for items that need good castability and mechanical performance. A357 can be utilized for some applications requiring some mechanical qualities depending on alloy specification and conditions of manufacturing. Other aluminum alloys are available where heat performance, pressure tightness, machinability, or cost is of greater importance.
Magnesium alloys are suitable for acceptable low-pressure casting applications, particularly where weight reduction is required. Protection is essential in the usage of melts, in handling, in oxidation, and in fire hazards. Other metals are generally not regarded as compatible and should be evaluated on a case-by-case basis in relation to machine setup, die materials, process temperatures, and production requirements.
Engineers should consider the casting properties and the performance following any heat treatment provided when selecting an alloy. A material that is OK in the lab may not be the best fit for commercial sale if it is difficult to cast reproducibly or does not meet the customer’s specifications after machining.
Designing Parts for Reliable Production
Decisions made in the pre-tooling design can greatly influence the casting quality and the production costs. The wall thickness needs to be as consistent as possible. The change from thick to thin is gradual. If the section thickness varies fast, the cooling will be nonuniform, and the tendency toward shrinkage faults will rise.
Ribs and bosses can offer stiffness and support for mounting features but must be designed with care for neighboring metal volume and heat build-up. Good and correct corner radii can enhance metal flow and reduce stress concentrations. Functional needs must be satisfied, but draft angles must be considered to allow the die to open and the casting to be removed.
Gates, vents, cooling channels, and separation lines should be seen as one, not as separate qualities. Also, the engineers need to define machining allowances, datum surfaces, sealing zones, and key parameters before the mold is finalized.
For complex components, design for manufacturing reviews and casting simulation can be utilized to identify potential difficulties of filling and solidification before completion of tooling for production. However, the simulation findings should be considered as technical advice and should be checked by the real casting tests and inspection results.
Improving Casting Quality and Preventing Defects
Understanding Porosity, Shrinkage, and Incomplete Filling
Porosity is one of the most important defects to consider in cast metal parts. Porosity of gas is caused by dissolved gases, impurities, or entrapped air and porosity of shrinkage when there is not enough liquid metal to compensate for the decrease in volume on solidification.
Low-pressure die casting is a controlled filling and feeding process that does not guarantee porosity-free castings. Results rely on melt preparation, die temperature, pressure holding, solidification behavior, and shape of thick sections.
Cold closures and incomplete fills arise when the metallic surfaces do not contact well or the metal is not fluid enough to fill the whole cavity. These difficulties can be caused by low metal temperature, insufficient venting, poor gate location, or wrong fill conditions.
Other concerns include oxide inclusions, surface defects, warping, and dimensional fluctuations. Each defect has to be evaluated according to its location, appearance, frequency, and significance to the manufacturing conditions. The main cause of a problem is usually alloy cleanliness, die design, or non-uniform cooling, which is rarely fixed by altering the pressure alone.
Establishing an Effective Inspection Plan
The function of the component and the risk of failure should dictate inspection requirements. Visual inspection can identify surface faults, glare, apparent cracks, and other handling issues. Dimensional inspection is to measure the main features to determine if they are within the tolerances specified on the drawing. Coordinate measurement equipment can measure complex geometries.
Where included in the product specification, interior discontinuities can be checked by X-ray or computed tomography examination. Depending on the service conditions expected for the housings, a pressure, fluid, and/or leak test may be required. If material qualities or internal structure are significant, mechanical testing and metallographic investigation can provide extra information.
The inspection methods to be used shall be determined by the acceptance criteria and the limitations of each approach. For example, the external visual inspection does not allow verification of the absence of pores in the inner structure. A dimensions report may be all that is required without showing a casting to be all mechanical specifications.
The quality plan calls for close association of inspection data with material lots, production records, process parameters, and component identification. This traceability is useful to producers to trace nonconformities, to validate corrective efforts, and to maintain a continuous quality of manufacturing.
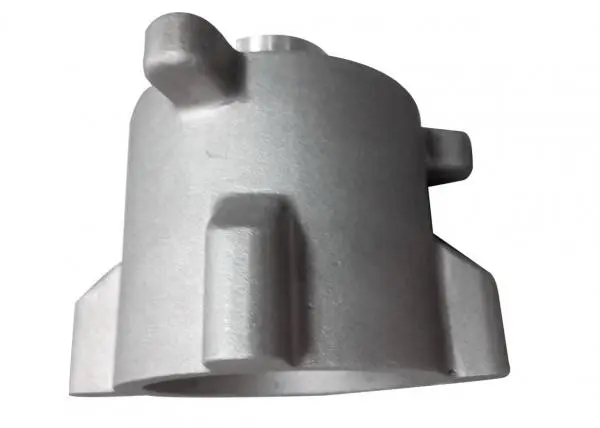
Heat Treatment, Machining, and Finishing
Post-Casting Operations and Their Effects
Some aluminum castings produced through low pressure die casting are heat-treated to give them certain mechanical properties. The T6 treatment commonly includes solution heat treatment, quenching, and artificial aging. The exact cycle is dependent on the alloy, section thickness, casting quality, and customer requirements.
The real part is to check the heat treatment. The tests above do not demonstrate any distortion or other difficulties inherent to excessive or inadequate processing. If dimensional stability is vital, the important parameters should be confirmed after heat treatment and not only on the basis of measurements in the as-cast condition.
The bearing seats, threaded holes, sealing faces, mounting interfaces, and other functional parts can be machined. The machining allowance must be adequate to permit the variation in the casting but not so great as to eliminate excess material. Machining procedures may bring inner porosity to the surface; therefore, it is vital to have inspection and acceptance criteria for crucial surfaces.
Surface finishing such as conversion coatings, painting, powder coating, or other treatments depending on the component service environment. Verification of surface preparation, coating thickness, adhesion, and corrosion performance as required by the function of the product.
Incorporating these downstream requirements into the original casting design helps reduce the amount of rework and late discovery in production that a casting will not meet its final dimensions or surface requirements.
Applications of Low-Pressure Die Casting
Transportation & automotive: Specific wheel designs, motor housings, structural components, and other items where controlled metal filling and consistent material distribution provide benefits. It is contingent upon the alloy, on the loading conditions, and on the safety requirements and laws of the vehicle or customer involved.
Electric vehicle motor housings and thermal-management components may require a balance of dimensional correctness, heat dissipation, sealing performance, and dependable machining interfaces. Engineers should be looking at the entire component standard and not a weight reduction-oriented strategy.
Where Low Pressure Die Casting Is Used?
Weight, material properties, dimensional uniformity, and traceability are key for airplane components. However, not all components for airplanes are suitable for low-pressure die casting. The design shall be in compliance with the applicable material and qualification criteria, and the production process shall be qualified for the intended purpose.
Cast housings, pump components, and other enclosures are used by industrial equipment makers where the geometry and reproducibility of manufacturing lend themselves to this technique. In case the components are subjected to pressure, vibration, cyclic loads, or a harsh operating environment, the validation shall be undertaken under real service circumstances.
Electrical and Thermal Management Products
Cast components are employed in electrical equipment, motor systems, and some communications devices as structural support, to dissipate heat, or as enclosures. The die design and the choice of metal affect the thermal and mechanical performance. The part is machined to the assembly specifications and polished.
The functional requirements of each application, the production volume, tooling costs, inspection needs, and the implications of any component failure all dictate the technique of choice.
Conclusion
Low-pressure die casting is a controlled process for organizations to make metal parts needing consistent fill, adequate mechanical properties, and predictable dimensional performance. Efficiency depends on alloy choice, die design, management of pressure and temperature, solidification, and downstream processing. The same attention must be taken with inspection and traceability when the demands for components are high.
For the engineers it is important to compare the casting process with other alternatives and to evaluate the product shape, the amount of production, the desired price, and the functional requirements so that they may choose the best alternative. Working with a competent supplier from the design phase can help decrease manufacturing risks and increase production consistency and can help map a more defined path from prototype validation to repeat orders.
Ready to discuss your pressure casting requirements? Contact us at steve.zhou@263.net and zhouyi@rongbaocasting.com to explore how our comprehensive manufacturing capabilities can support your next project development.
Pressure casting technology offers manufacturers exceptional capabilities for producing high-quality components across diverse industrial applications. The process combines controlled pressure application with sophisticated automation to deliver consistent results meeting stringent quality requirements. Success depends on proper material selection, optimized process parameters, and comprehensive quality control measures. As industries continue demanding lighter, stronger, and more complex components, pressure casting remains an essential manufacturing technology for achieving these objectives while maintaining cost-effectiveness and production efficiency.
References
- Campbell, J. "Complete Casting Handbook: Metal Casting Processes, Metallurgy, Techniques and Design." 2nd Edition, Butterworth-Heinemann, 2015.
- Ravi, B. "Casting Simulation and Optimization: Benefits, Bottlenecks and Breakthroughs." Indian Foundry Journal, Vol. 54, 2008.
- Flemings, M.C. "Solidification Processing in Metal Casting and Continuous Casting." Materials Science and Engineering A, Vol. 178, 1994.
- ASM International. "Casting: ASM Handbook Volume 15." ASM International Materials Park, 2008.
- Bonollo, F., Urban, J., Bonatto, B., and Botter, M. "Gravity and Low Pressure Die Casting of Aluminium Alloys: A Technical and Economical Benchmark." La Metallurgia Italiana, Vol. 97, 2005.
- Zhang, L., Damoah, L.N.W., and Robertson, D.G. "Removal of Inclusions from Aluminum through Filtration." Metallurgical and Materials Transactions B, Vol. 43, 2012.